| Availability: | |
|---|---|
| Quantity: | |
70 screw, 2 stations, 1 cavity
Buck machine
Machine Introduction
This machine is a **70 screw fully automatic servo hydraulic 2-station 1-cavity hollow blow molding equipment**. It is specially designed for the mass production of HDPE, PP and other plastic hollow products. It adopts servo hydraulic drive + double-station rotation molding structure, single mold 1 The cavity layout takes into account stable production capacity and energy consumption control, and is suitable for the production of various types of single-layer hollow containers such as chemical barrels, oil bottles, and daily chemical bottles. The equipment has a high degree of automation and is easy to change. It is the preferred model for the large-scale production of small and medium-sized hollow products.
| 螺杆 screw | 70MM |
| 最大容量 Max. product volume | 5L |
外形尺寸 size | 3640*2000*2200MM |
机器重量 weight | 4.5T |
塑化能力 Plasticizing ability | 65Kg/H |
加热功率 Heating power | 13.2KW/H |
挤料电机 Extrusion motor | 15KW |
油泵电机 Oil pump motor | 15KW |
减速器 reducer | 173 Hardened tooth surface, high strength,low noise and anti-wear reducer |
模板尺寸 Template size | 450*450MM |
锁模力Clamping force | 100KN |
| 中心距 center distance | 0 |
Machine head
Center feed die head
Mould opening and closing mechanism
Hydraulic mold clamping, Hydraulic mold shifting

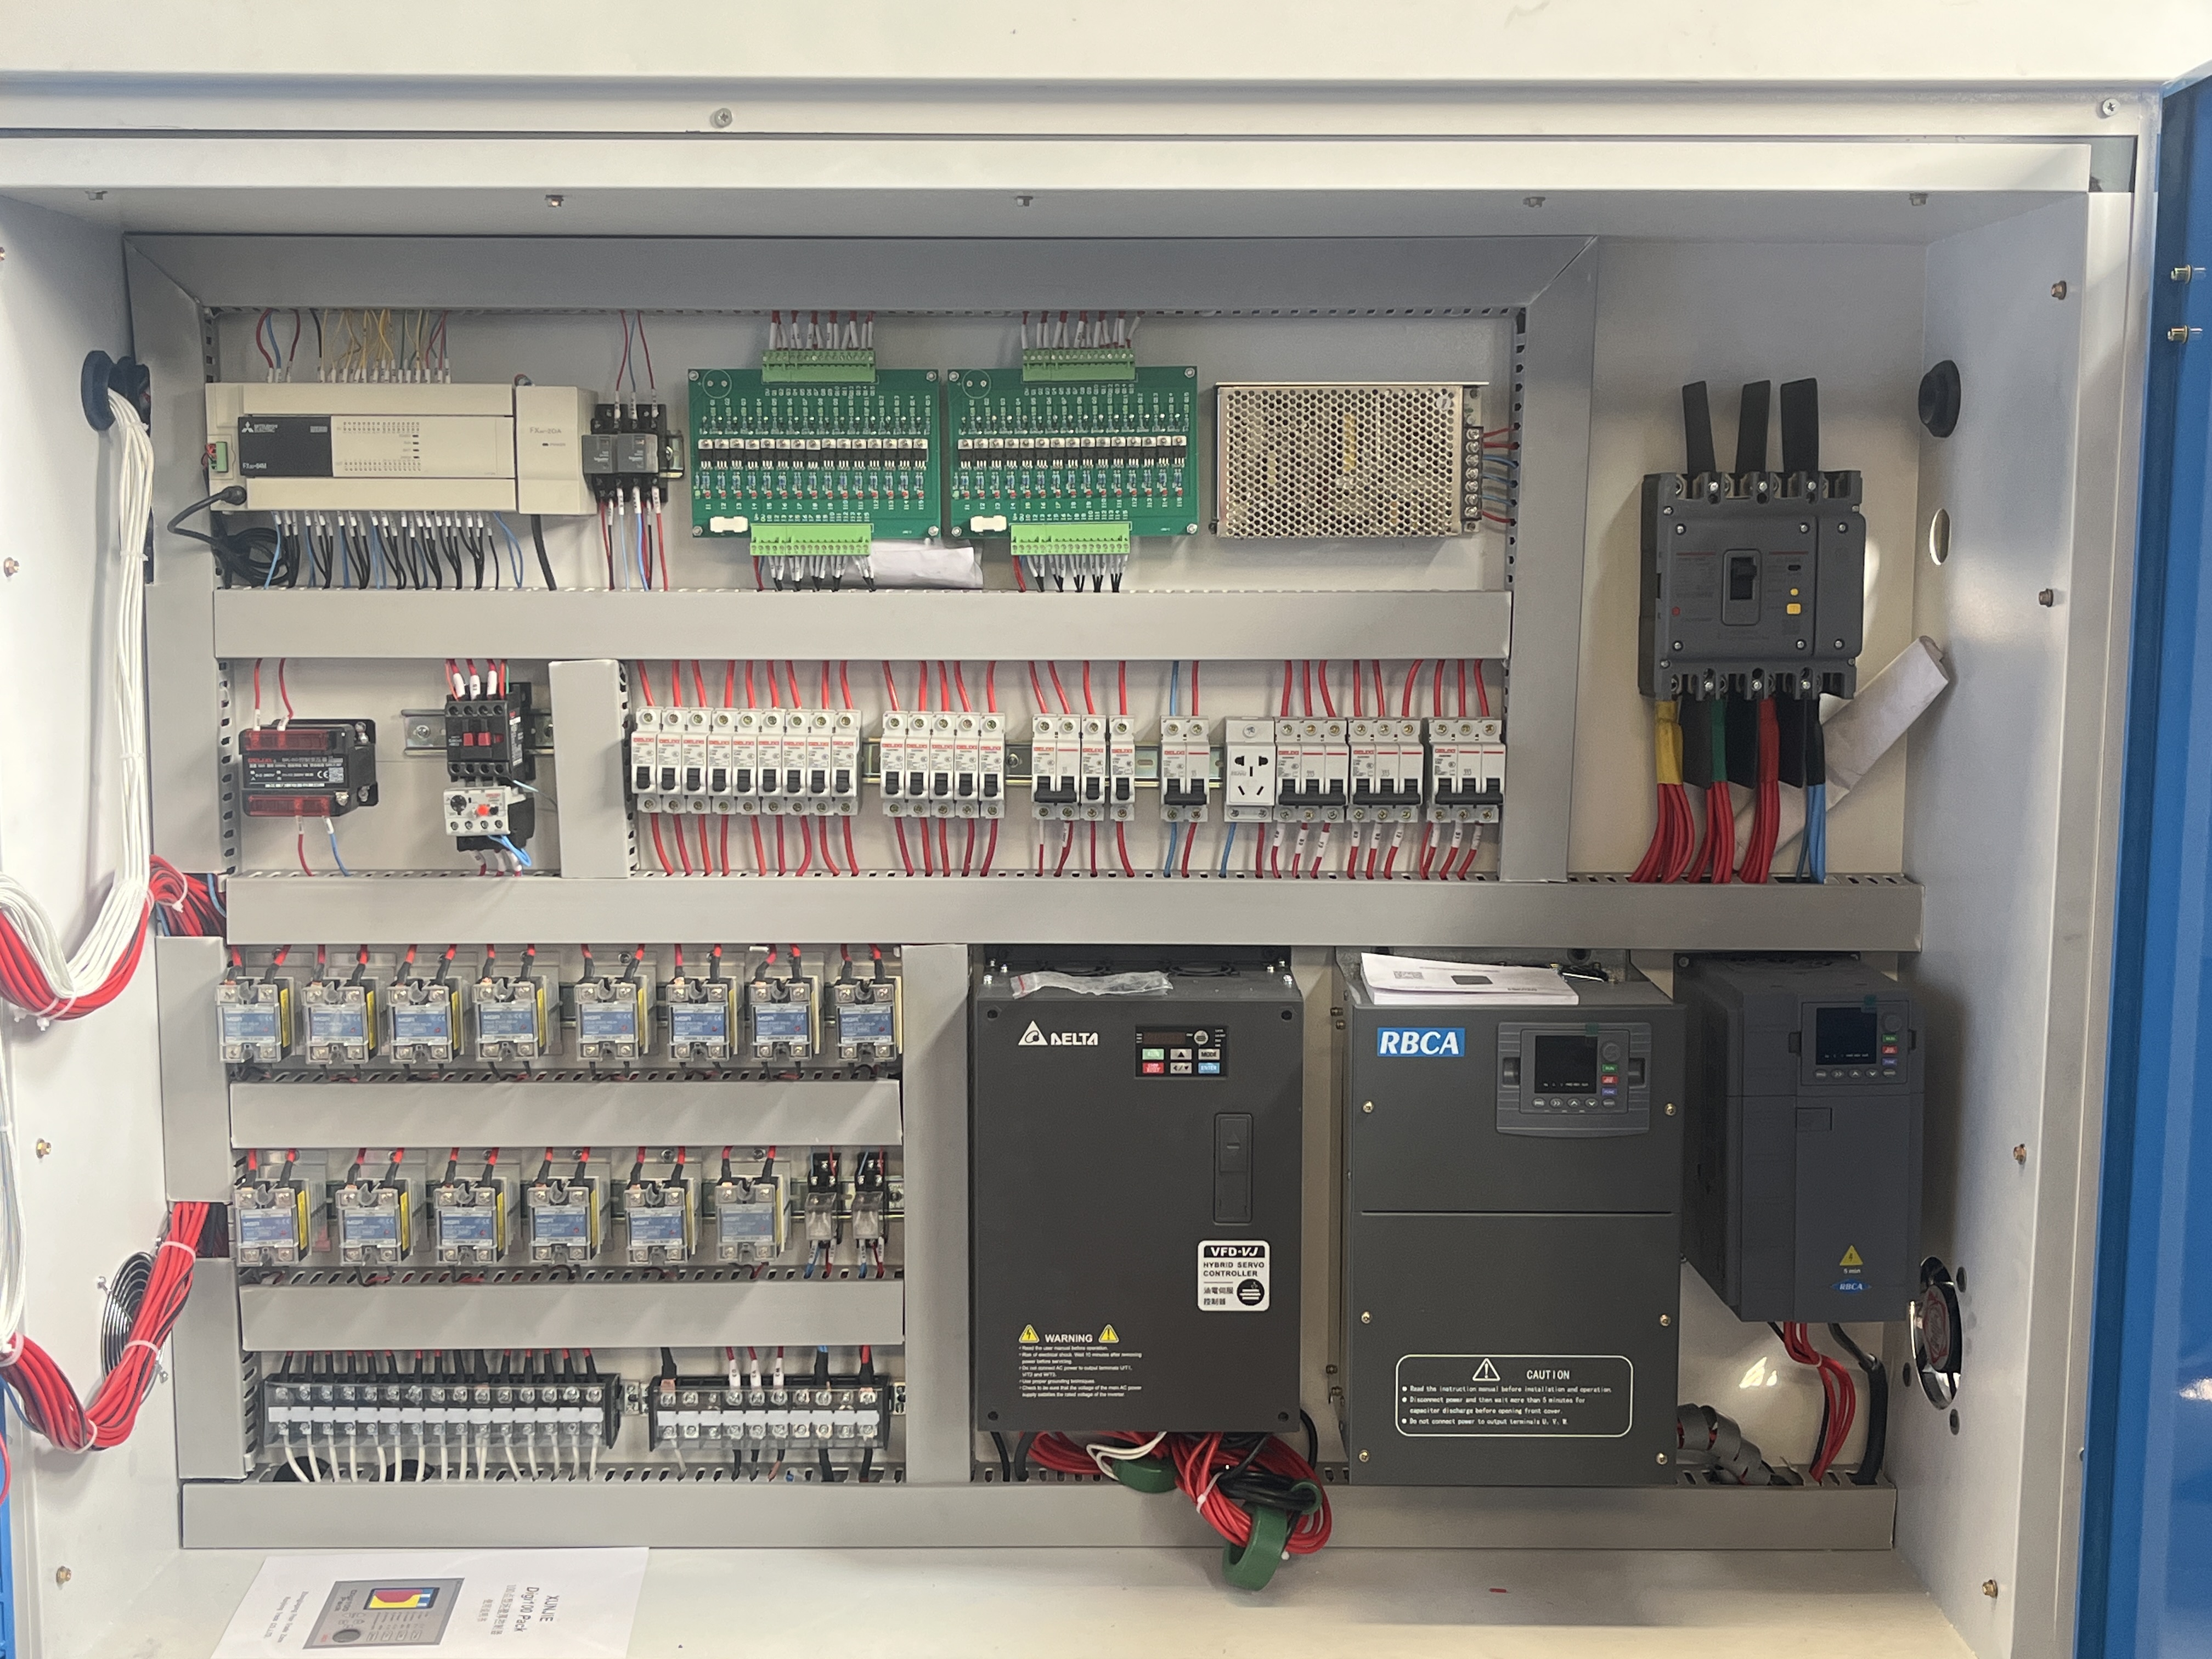
Electric box
Screw heating,
nitriding steel 38CrMoAlA
5 Cast aluminum heating coil
Mitsubishi PLC Touch Screen
Temperature controller
Automatic de flash device
The machine can add automatic de flash function to reduce labor costs
Servo system Inverter
Delta from Taiwan
RBCA Inverter
1. Extrusion System: Φ70 Screw
A dedicated Φ70 compounding screw with optimized screw thread structure ensures uniform plasticization and stable output, suitable for HDPE/PP raw materials; segmented barrel temperature control with an accuracy of ±1℃ ensures high consistency in melt density, reducing thickness fluctuations, and is suitable for mixed production of recycled and virgin materials.
2. Drive Method: Servo Hydraulic System
A servo motor drives the hydraulic pump, outputting pressure and flow on demand, saving 25%~35% of energy compared to conventional quantitative pump hydraulic presses; fast hydraulic response, stable pressure, low noise, and smooth mold clamping action extend mold life.
3. Molding Structure: 2 Stations, 1 Cavity
Dual-station alternating cycle (one station for blow molding, the other for part removal and preform placement) allows for uninterrupted continuous production; the single-mold, 1-cavity design concentrates clamping force, resulting in uniform product wall thickness, suitable for container products with high requirements for appearance and sealing.
4. Control System: Fully Automatic PLC Human-Machine Interface
The entire machine is centrally controlled by a PLC, with a color touch screen operation; it supports wall thickness curve setting, one-click parameter storage and retrieval, fault self-diagnosis alarm, easy for beginners to use, fully automated, and manual handling is only required for simple part removal.
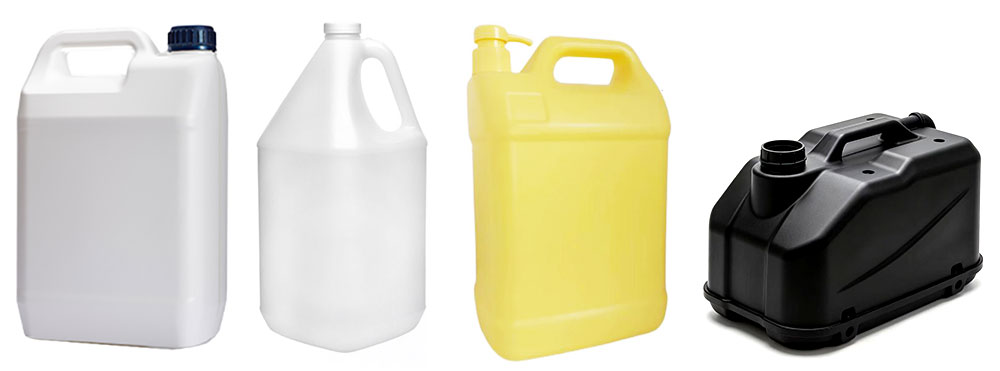
This versatile machine is well-suited for manufacturing a wide range of hollow products, including:
Plastic bottles (for beverages, daily chemicals, and pharmaceuticals)
Containers and canisters
Industrial hollow components
Household plastic goods
With its combination of high throughput, precision molding, and operational stability, our Dual-Station 1-Cavity Blow Molding Machine is the ideal choice for manufacturers seeking to enhance production efficiency and product quality.
Click here to edit your content.

Cangzhou Buck Machinery Manufacturing Co., Ltd. is a professional export-oriented company specializing in the research, development, production, and sales of fully automatic and semi-automatic electric blow molding machines.
We mainly produces a full range of efficient, energy-saving, and highly stable blow molding equipment, covering small, medium, and large models. It can manufacture plastic bottles and hollow plastic products from materials like HDPE, PP, and PET, widely used in daily chemicals, beverages, food, pharmaceuticals, industrial packaging, and household goods.
We provide global customers with one-stop services including equipment customization, mold development, on-site installation guidance, and lifetime after-sales technical support. With excellent product quality, competitive factory prices, and thoughtful foreign trade services, we have been deeply cultivating overseas markets for many years.
Q: How to choose between fully‑automatic and semi‑automatic blow molding machines?
A: Choose semi‑automatic for small‑batch production, limited budget and frequently‑changed product specifications. Choose fully‑automatic for mass‑volume production, labor saving and stable continuous output. A semi‑automatic machine requires 1‑2 workers for part taking and trimming, while the fully‑automatic model supports near‑unmanned operation.
Q: What products are suitable for accumulator‑head blow molding machines?
A: It is mainly used for large‑capacity hollow articles, such as 20L‑200L chemical drums, water tanks, amusement parts and automotive plastic components. It fits heavy‑weight thick‑wall products which ordinary machines cannot produce.
Q: What plastic materials can the blow molding machine process?
A: Main materials: HDPE, PP. Some models support LDPE and EVA. For PET bottles, injection‑blow integrated machines are recommended; ordinary hollow blow molding machines are not ideal for PET processing.
Q: What auxiliary machines are required for a blow molding unit?
A: Chiller, screw air compressor, auto loader, material mixer and plastic crusher. Optional equipment includes mold temperature controller and material dryer based on raw materials and output requirements.
Q: Which machine is suitable for 1‑5L plastic bottles?
A: Medium‑small fully‑automatic blow molding machines are recommended for 1‑5L daily‑chemical bottles and oil bottles. Multi‑cavity molds can be matched to improve production capacity.
Q: What causes uneven wall thickness of finished parts?
A: ① Improper die head gap adjustment; ② Unstable parison extrusion speed; ③ Raw material temperature fluctuation; ④ Inconsistent mold cooling performance; ⑤ Unstable extrusion pressure of accumulator head.
Q: How to solve air‑bubble defects on blow‑molded products?
A: Dry damp raw materials; reduce barrel temperature to avoid material decomposition; check screw compression ratio; remove moisture and impurities inside raw materials.
Q: Obvious parting line and large flash on products, how to fix?
A: Insufficient clamping force; worn mold parting surface; excessive clearance of clamping mechanism; excessive parison material volume.
Q: Products cannot be fully blown out or have local depressions?
A: Insufficient blowing air pressure; blocked blowing nozzle; over‑fast mold cooling; too‑short parison; blocked mold exhaust holes.
Q: Difficult demolding, plastic sticking to mold cavity?
A: Excessively high mold temperature; insufficient draft angle; rough mold cavity surface; over‑high raw material temperature; appropriate release agent can be added.
Q: What pre‑start‑up inspections shall be done for new machines?
A: Check hydraulic oil level, air compressor pressure and chiller water circulation; confirm mold fastening; keep heating zones at target temperature for 30‑minute heat preservation; perform dry clamping test before feeding raw materials.
Q: What to do if hydraulic oil temperature is too high?
A: Check cooling performance of chiller; replace aged hydraulic oil; reduce excessive relief‑valve pressure; avoid long‑time non‑stop running. Replace hydraulic oil periodically.
Q: Daily maintenance for screw and barrel?
A: Clean barrel thoroughly when switching raw materials; lower temperature for long‑time shutdown; prevent metal hard objects from entering feeding port to avoid screw scratch; inspect wear clearance regularly.
Q: How often to sharpen crusher blades?
A: Inspect blades every 2‑3 months under normal production. Sharpen blunt blades timely. Over‑large crushed particles will harm finished product quality.
Q: Frequent alarm of chiller, root causes?
A: Filter blocked by impurities in cooling water; insufficient water level; dust‑covered condenser; excessive ambient temperature; blocked circulating pipeline.
Q: What is your machine lead time?
A: 30‑45 working days for standard models; 45‑60 working days for customized and accumulator‑head models, excluding sea freight time.
Q: Can the machine match our local voltage?
A: Yes. Voltage and frequency can be customized according to clients’ local power grid for motors and electric control system.
Q: Do you supply molds? What is mold service life?
A: Custom‑developed molds are available. Aluminum alloy molds: hundreds of thousands shots; steel molds: more than one million shots, subject to products and raw materials.
Q: What services are included for exported machines?
A: Pre‑shipment inspection & testing; English operation manual; remote video guidance for installation & commissioning; oversea on‑site technical service available (travel expenses borne by buyer); lifetime technical after‑sales support.
Q: What is the warranty period?
A: 12‑month whole‑machine warranty. Wearing parts (blades, sealing rings, heater bands) are excluded from warranty. Original spare parts can be supplied continuously after warranty expiration.
Q: How much floor space does the machine need? How large workshop is required?
A: Medium‑small fully‑automatic machine occupies about 6‑10 ㎡. Large accumulator‑head machines need larger space. Extra space shall be reserved for auxiliary machines and finished‑goods turnover. You may send your site dimension for our layout suggestion.
